
Turnkey Plant for Maltitol Production
From Starch to High-Purity Maltitol—One Integrated Production Solution
As food manufacturers reformulate products with less sugar, maltitol has become an important sugar alcohol for sugar-free and reduced-sugar confectionery, bakery products, chocolate, oral care and pharmaceutical applications. Its sweetness profile, functional properties and processing stability make it particularly valuable where manufacturers need more than sweetness alone.
For maltitol producers, however, consistent product quality starts long before hydrogenation.
The maltose composition of the syrup, impurity level, hydrogenation conditions, catalyst performance, purification efficiency and evaporation system all influence final maltitol purity, color, stability, production cost and plant reliability. Poor integration between these stages can lead to inconsistent conversion, higher catalyst consumption, greater energy demand and difficulty maintaining the required product specification.
Myande Maltitol Production Solution
Myande provides complete maltitol production plants integrating:
Starch Slurry Preparation → Liquefaction → Saccharification → Purification → Hydrogenation → Refining → Evaporation → Maltitol Syrup
For projects starting with maltose syrup, the production line can also be configured from syrup purification and hydrogenation onward.
Backed by more than 23 years of experience in starch sugar processing, equipment manufacturing and turnkey engineering, Myande designs each plant around the customer's raw material, target maltitol specification, production capacity and utility conditions.
Our scope can cover process engineering, 3D plant design, equipment manufacturing, automation, installation and commissioning guidance, operator training and after-sales service.


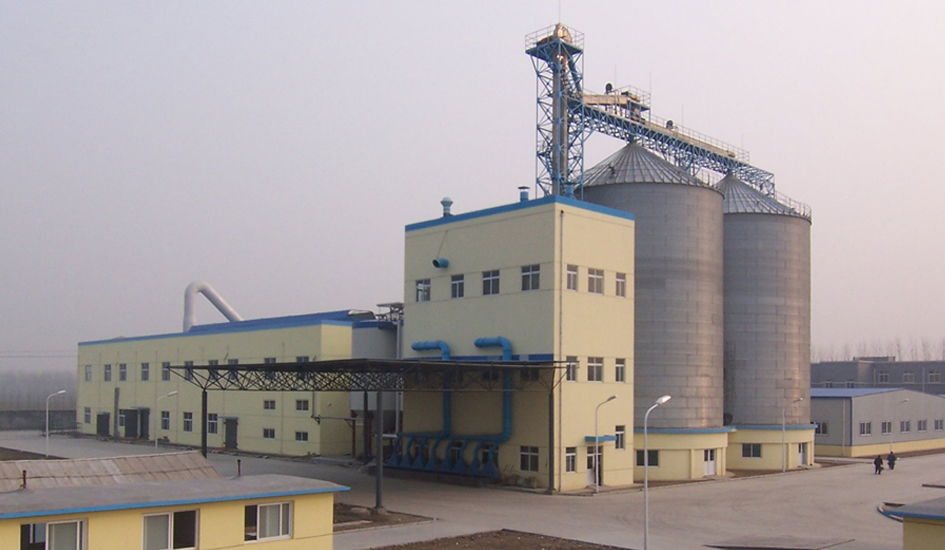
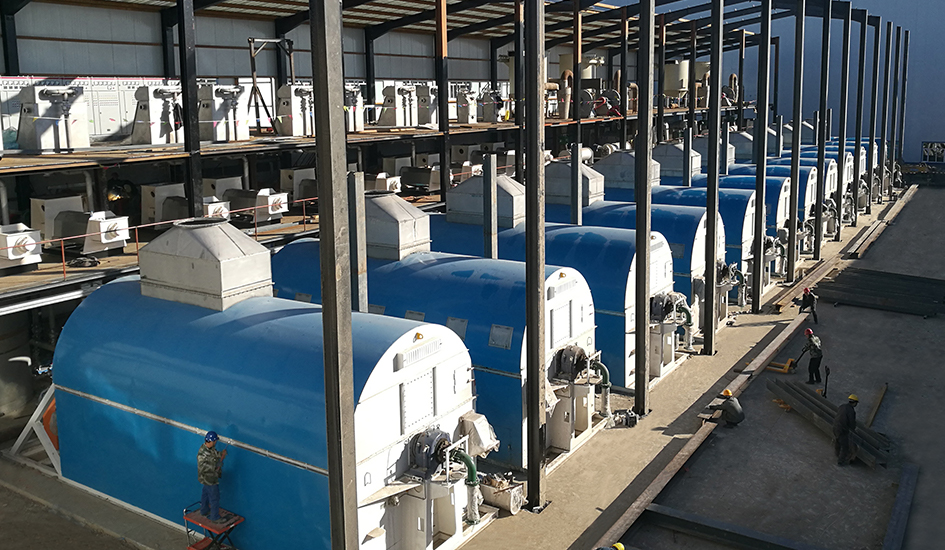
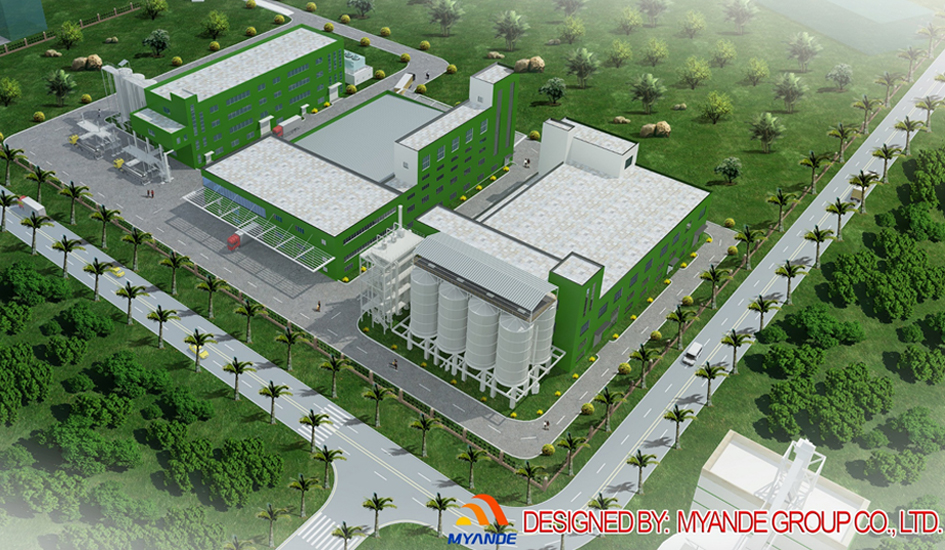
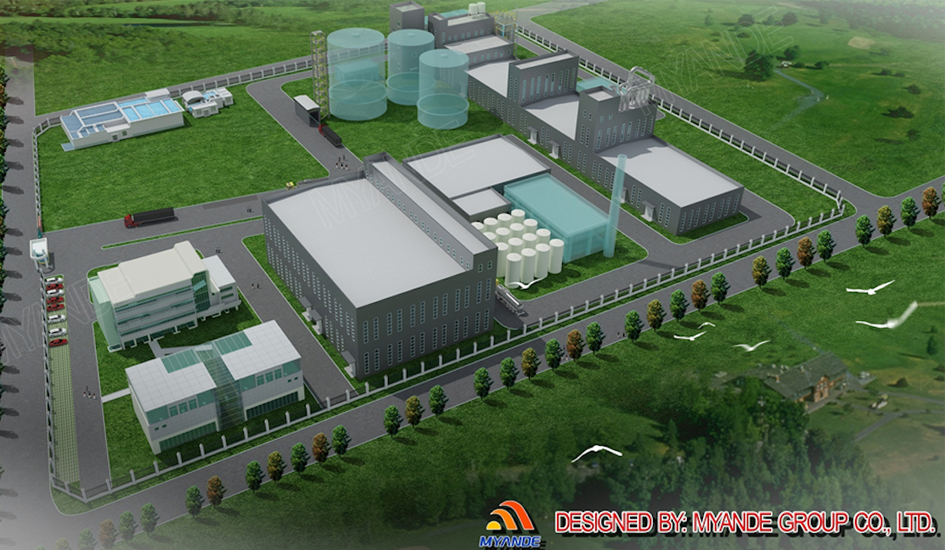
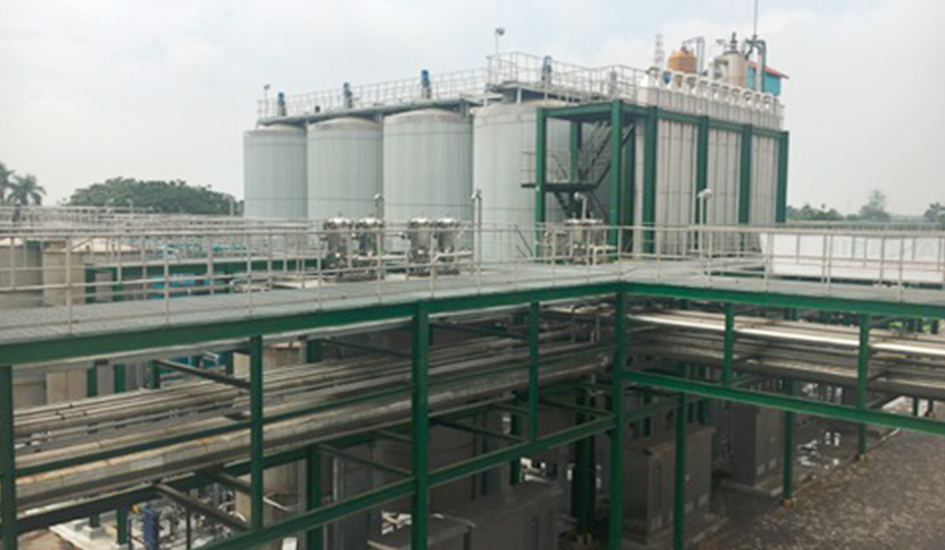

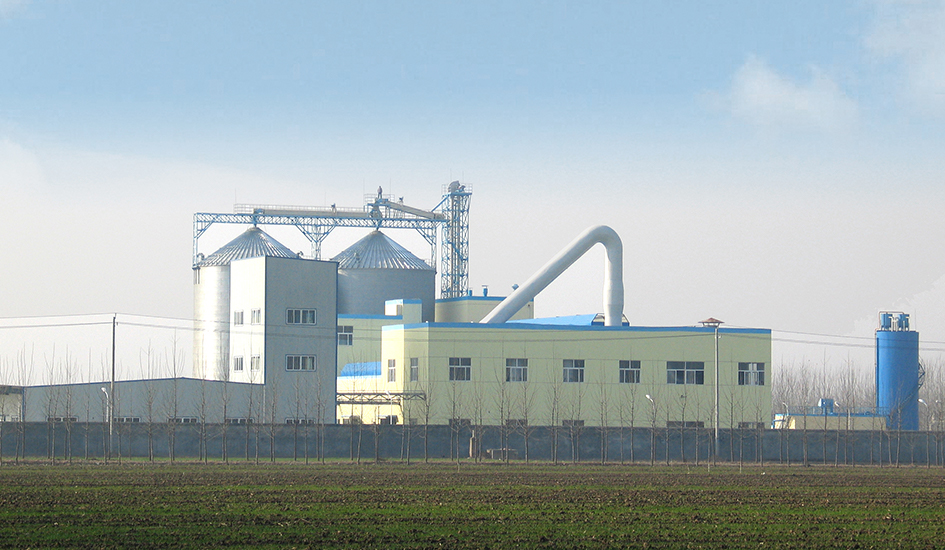
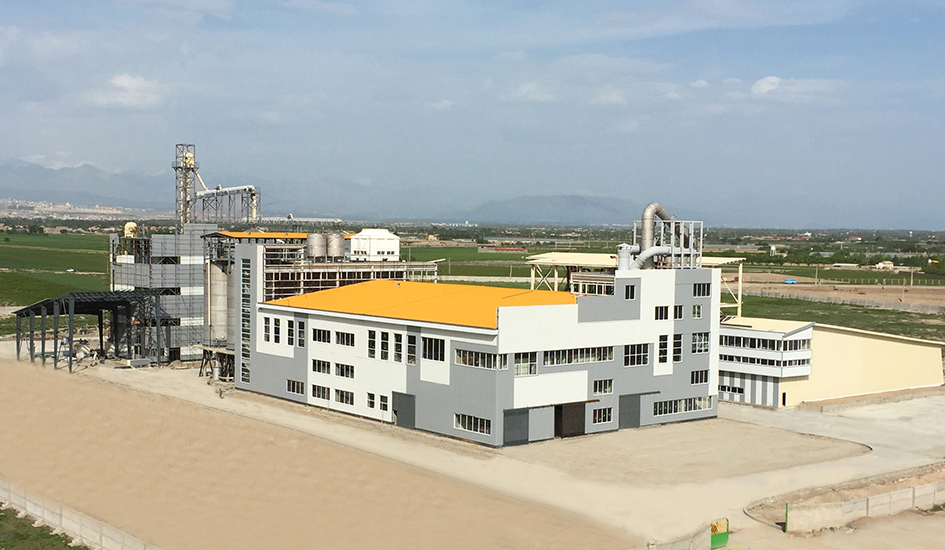
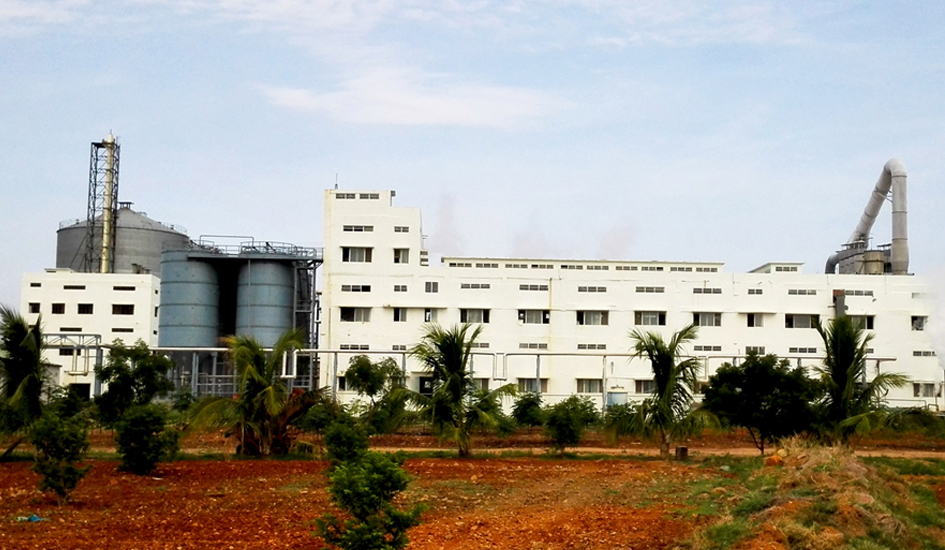
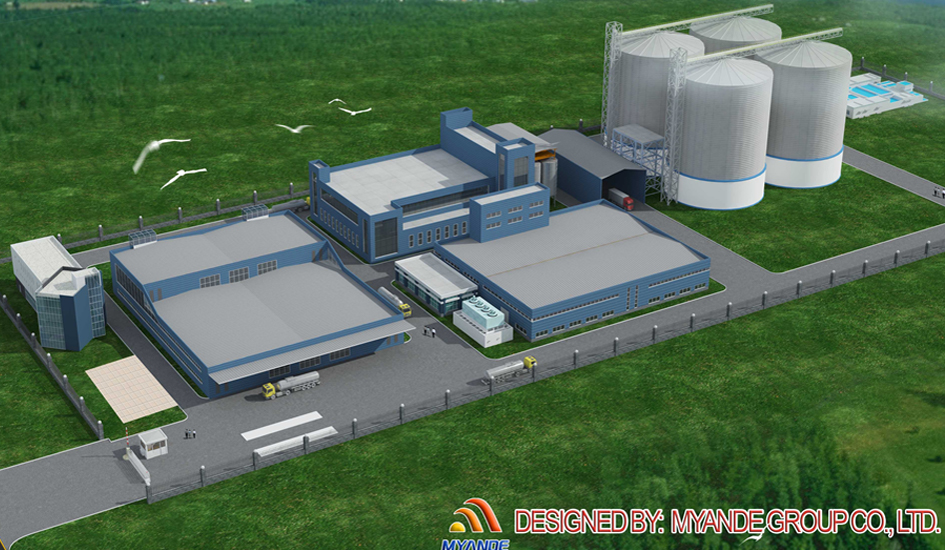
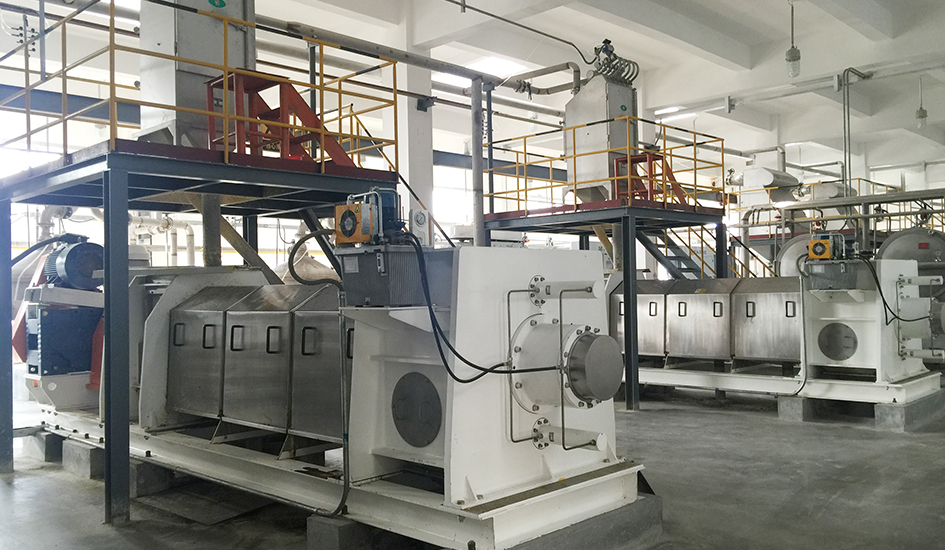
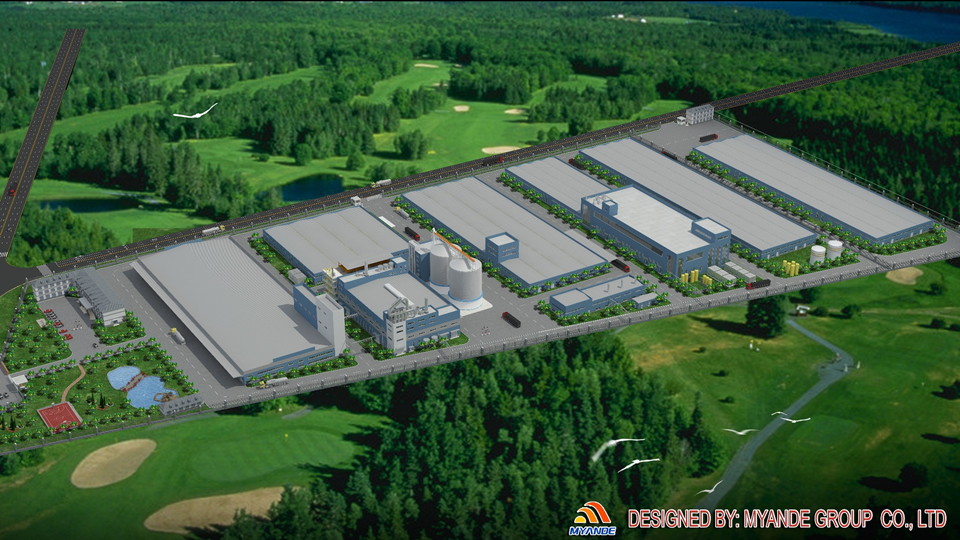

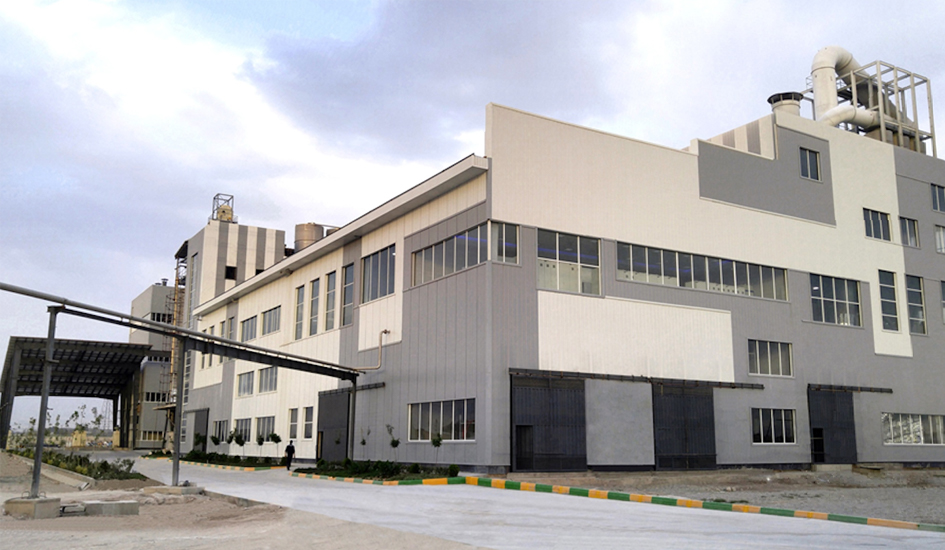
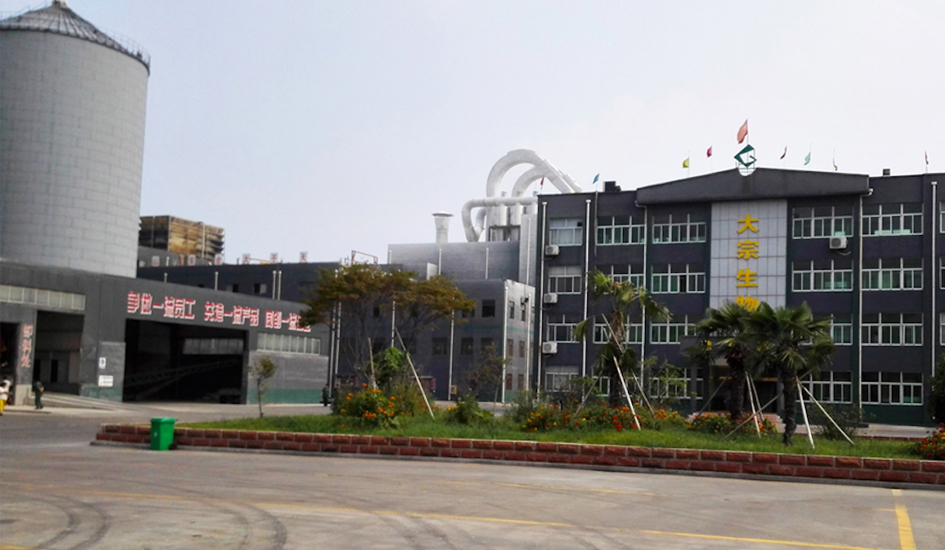
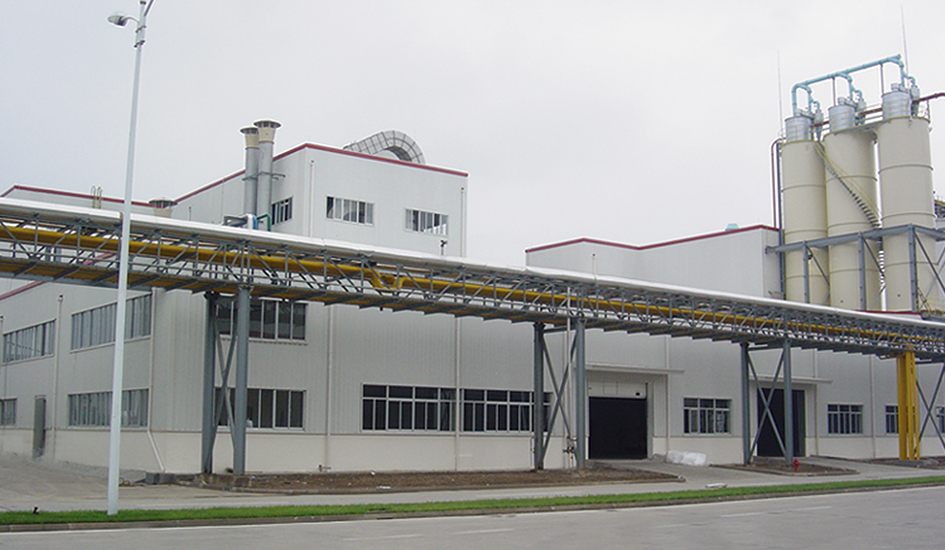
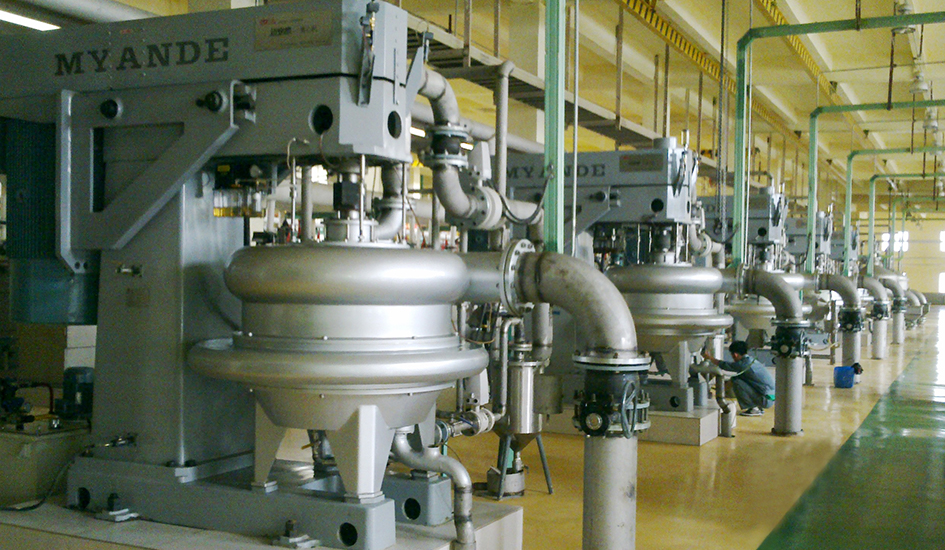
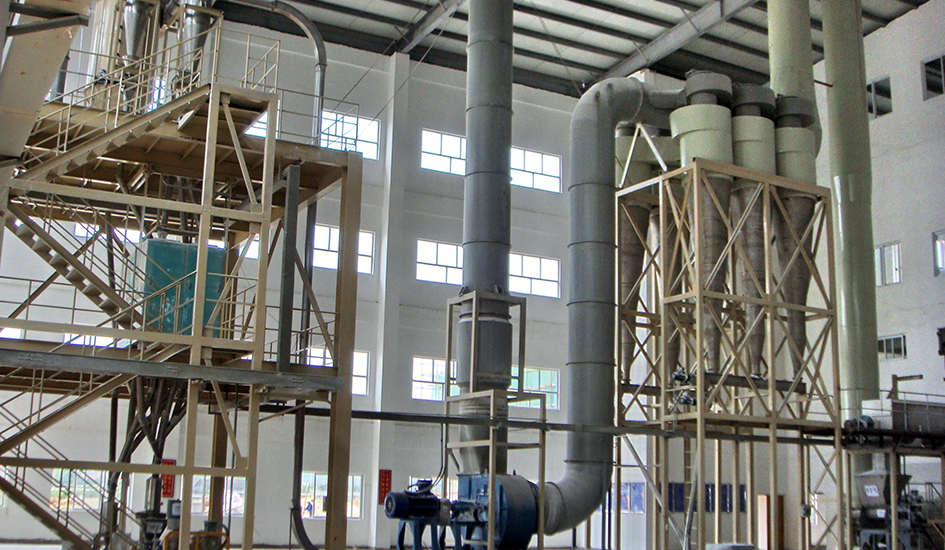
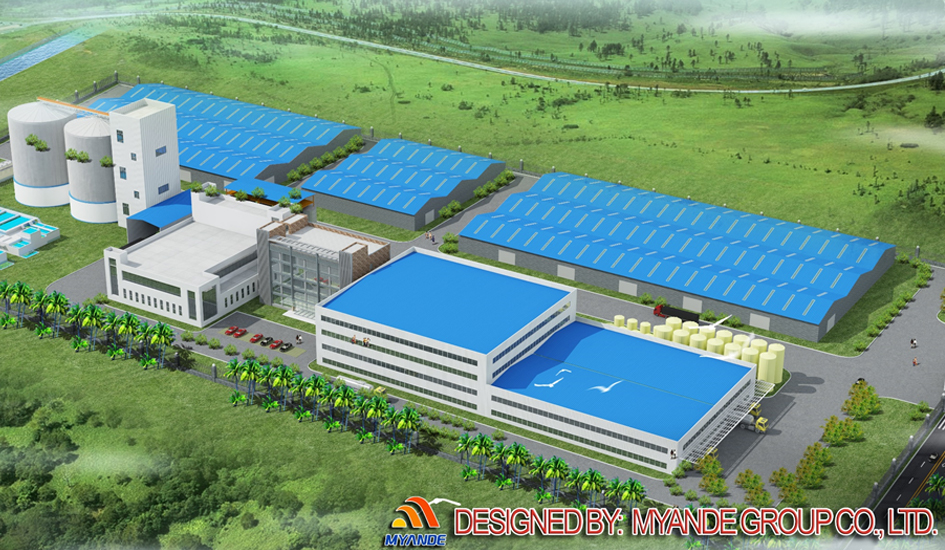

Complete Process. Zero Hassle. From Starch to Maltitol.
Our turnkey solution covers the full maltitol production process:
1. Liquefaction & Saccharification
Raw starch is liquefied and enzymatically treated to produce maltose-rich syrup.
2. Hydrogenation
The syrup undergoes catalytic hydrogenation in our high-pressure, safe-reactor systems.
3. Refining & Purification
Myande’s multi-stage filtration, ion-exchange and evaporation units ensure high purity.
4. Crystallization or Spray Drying (Optional)
For solid maltitol applications, we offer crystallization and drying systems with advanced control.
Each process step is optimized for energy savings, minimal product loss, and easy CIP (Clean-in-Place) maintenance.

What Sets Myande Apart in Maltitol Production Solutions
✅ Consistent Maltitol Purity
Control the process from maltose syrup preparation through hydrogenation and final purification.
✅ Stable Hydrogenation
Optimize feed quality and reaction conditions to support efficient conversion and reliable catalyst performance.
✅ Lower Energy Consumption
Integrate heat recovery and efficient evaporation technologies to reduce the thermal demand of concentration.
✅ Food-Grade Production
Design hygienic process systems around the required product and applicable market standards.
✅ Flexible Plant Configuration
Build from starch or integrate with an existing maltose syrup production line according to the project.
✅ Reliable Continuous Operation
Combine process design, equipment, instrumentation and automation into one coordinated production system.

They trust and choose Myande
More than 1,600 complete plants have been supplied under Myande’s name in over 80 countries since 2003.
Behind every successful project is a great team. Our team is comprised of skilled individuals that share one common goal – Help our clients succeed.

What can we do for you?
We focus on supplying one-stop engineering service covering general layout plan, process design, R&D, equipment manufacturing, automatic control system, data integration, installation, supervision, commissioning, training and etc.
Our custom solutions come from a deep understanding of your needs, and we have the capability to complete each project from the design of the initial concept to manufacturing, installation, commissioning and delivery.
Solution Tailored to Your Needs

General Layout Plan
With a land prepared, the next thing you should consider is planning the general layout, which is a crucial foundation of a sustainable and cost-effective manufacturing.
Turn to us for help and we will present you the design for your plant by considering water, steam, electricity supply and etc.

Process Design
Combining our engineering expertise, industry know-how and practical skills with your knowledge, we provide the optimized and customized process design for your plant.

3D Plant Design
On the basis of plant layout design, combined with real situation, we can design a three-dimensional model of the entire plant. All the equipment, piping and instruments, any detail can be shown in the model, not only allowing you to have an intuitive understanding of the plant, but also providing overall information support for plant construction, equipment installation and future expansion.

Automatic Control System
We offer economical and most effective process automation solutions for the entire production line. Our RES automatic control system is developed based on PLC/DCS system.

Data Integration
From the perspective of the overall operation of the factory, Myande intelligent data integration management system collects basic data from raw grain procurement, warehousing, processing, inventory, sales and logistics, relying on the interconnection network system of each workshop. It provides real-time, accurate and traceable data reports for the current storage, processing and shipping.

Equipment Manufacturing
We owns in-house manufacture base of more than 130,000㎡ integrating R&D, production, project management which represents advanced engineering capability in the industry.

Installation and Commissioning
After finishing the installation of all machines, we offer on-site commissioning service to ensure compatible functioning.
Every move of the machine needs strong technical support from our experienced engineers. The only principle is that you can start manufacturing right after the commissioning.

Training and After-sales Service
Myande 360° Service Portfolio covers all your needs throughout the life cycle of your project. By minimizing your total cost of ownership, we help you stay ahead of the competition.
About Myande
Myande Group is a globally leading supplier of complete plants, equipment, and services for Oils & Fats, Starch & Derivatives, Fermentation, Evaporation & Crystallization, Material Storage and Handling and Smart Factory industries.
Myande Group currently has 1,600+ employees including 800 technical staff and 800 manufacturing workers. More than 1,600 complete plants have been supplied under Myande’s name in over 80 countries since 2003.
World-leading manufacturing base
In-house manufacture base of more than 130,000㎡ that integrates R&D, production, and project management, representing world-class engineering capability in the industry.

No Compromise on Quality
We are highly committed to Quality Assurance.
Our facilities and processes adhere to the highest local and international industry standards and certifications and are audited regularly for compliance.
With a global quality management system, we ensure that our customers all over the world receive high-quality, reliable products and solutions. We are well aware that our equipment have to function safely and efficiently for decades.
To effectively carry on the spirit of artisanship, improve the overall quality of front-line employees, we hold the “Workmanship Skills Competition" every year.


Certificates & Patents
At Myande, innovation is the result of the total process of developing an idea into a product or a new way of working which adds value to the business.
Over 600 registered patents and utility models demonstrate the company's innovation potential.

Our Global Presence
We focus on supplying one-stop engineering service covering general layout plan, process design, R&D, equipment manufacturing, automatic control system, data integration, installation, supervision, commissioning, training and etc.
Our custom solutions come from a deep understanding of your needs, and we have the capability to complete each project from the design of the initial concept to manufacturing, installation, commissioning and delivery.
You might also be interested in


Related Products


Lifecycle Service
Technical expertise and innovative products form the basis of your success. But we offer you even more: our extensive range of services gives you optimum support for your requirements and objectives in the long term.
Myande News & Insights

2,000TPD Rapeseed Crushing Plant Launched
Recently, a 2,000 t/d rapeseed crushing plant built by Myande Group for Daodaoquan Grain and Oil Co., Ltd. started operation successfully and started to yield qualified rapeseed oil and meal. Daodaoquan Grain and Oil Co., Ltd. is a comprehensive oil processing enterprise integrating production, scientific research, trade, warehousing and logistics of edible vegetable oil and its related by-products. This new rapeseed crushing plant incorporates a wide range of Myande core equipment possessing independent intellectual property rights, including the E-type extractor, hydraulic flaker, DTDC, conditioner, and other key equipment. To achieve flexible material incoming and discharging, Myande CCJL series sweep auger and CQJL series reclaimer are used. In addition, advanced energy-saving technology, negative pressure draining technology and intelligent safety technology are used to ensure the stable operation of the entire production line and excellent product index. With the concept of "creating the best performance for our customers", Myande cooperates with DaoDaoQuan to build a modern, energy-efficient, and environmentally friendly factory.

600,000 T/A Wheat Starch Deep Processing Project Successfully Launched
Recently, the 1st phase of Henan Hanyong's 600,000 tons (annual output) wheat starch deep processing project, designed by and installed under the guidance of Myande, has been smoothly commissioned, and contract for the 2nd phase was signed with Myande, marking the further extension of the domestic wheat deep processing industry chain. Henan Hanyong Biotechnology Co., Ltd. is one of the leading enterprises in agricultural industrialization of Henan province. It mainly produces edible alcohol with strong competitiveness and a high reputation in the market. Starch deep processing is one of Myande’s important business segments. After years of technology and experience accumulation in the field of starch deep processing, Myande has formed a complete set of production design system with a high degree of automation, stable operation and high product quality. In recent years, Myande has successfully established long-term strategic cooperative relations with multiple famous domestic and international enterprises. Combining with Hanyong's own industrial advantages, after in-depth research, efficient communication and repeated demonstrations, Myande has designed a set of production plan (as shown in the following figure) specially for the customer, and it can not only produce gluten and wheat starch, but also make better use of the mixed nutrient solution of process water and pentosan to produce alcohol, which will bring considerable economic benefits. The 1st phase project is a 500tpd wheat flour processing project, including a 3tpd gluten drying system and a 12tpd starch drying system. From beginning to end, the whole project lasted for 10 months. During the whole implementation process, from the plant layout planning, process design, intelligent automation design in the early stage, project service in the mid-term, to the installation, commissioning and training in the post stage, Myande’s rigorous, attentive and efficient one-stop service has won the unanimous praise of Hanyong. Through the joint efforts of Myande and Hanyong employees, a brand-new starch deep processing production line was successfully commissioned and started running smoothly, and all indicators were superior to the technical level of the same industry. In view of the pleasant cooperation in the 1st phase, Hanyong decided to cooperate with Myande again to expand its wheat starch deep processing output, and signed the 2nd phase project with Myande resolutely, namely 5t/d gluten drying system and 20t/h starch drying system. After which, Hanyong will become a high-quality gluten high-value conversion base with "the largest scale, the best environment protection and the highest level of research and development" in the industry in Asia.

Myande Awards 2022 “Spring Sunshine” Scholarship
In order to motivate employees' children to study hard and to enhance employees’ sense of belonging and happiness, on August 19, Myande held 2022 Myande Spring Sunshine Education Scholarship ceremony. Mr. Wangmu, vice chairman and Mr. Mao Weijiang, director in charge of manufacturing, participated in this ceremony and on behalf of the company presented scholarship stipends to children of Myande employees who are enrolled by four-year universities this year. In his speech, Mr. Wang highlighted that Spring Sunshine Scholarship is one of several company welfare benefits. It represents the company’s vision of moving forward with its employees and creating a better future together, and it reflects the company's care for the education of its employees' children and its high sense of social responsibility.
FAQ
-
What should I evaluate before investing in a maltitol production plant?
-
Start with the target maltitol product and downstream market, not just plant capacity.
Maltitol syrup and crystalline maltitol have different requirements for maltose feed quality, hydrogenation selectivity, purification, concentration, crystallization, and finishing.
Investors should evaluate feedstock availability, target maltitol content, product form, hydrogenation performance, catalyst consumption, hydrogen consumption, overall product recovery, utilities, and target applications before finalizing the process.
The most meaningful KPI is the cost per ton of qualified, saleable maltitol at the required grade.
-
-
Why is high-maltose syrup quality critical to maltitol production?
-
Maltitol is produced by hydrogenating maltose, so the carbohydrate composition entering hydrogenation has a direct impact on final product composition.
A poorly controlled starch-to-maltose process can introduce excessive glucose, higher saccharides, salts, color-forming substances, and other impurities. These may increase hydrogenation by-products, purification requirements, or catalyst burden.
The production line should therefore optimize starch conversion, maltose formation, syrup purification, and hydrogenation as one connected process, rather than treating maltose syrup as a generic feedstock.
-
-
Why are hydrogenation selectivity and by-product control important?
-
High conversion does not automatically mean high maltitol yield.
Hydrogenation conditions can affect the formation of unwanted products such as sorbitol and other components, which may reduce maltitol purity and increase downstream purification costs.
Reaction temperature, pressure, hydrogen availability, feed composition, catalyst contact, residence time, and process stability therefore need to be optimized together.
For industrial plants, maltitol selectivity and qualified-product recovery are more meaningful than hydrogenation conversion alone.
-
-
How can a maltitol plant reduce sorbitol and other unwanted polyols?
-
The first step is to control the carbohydrate composition of the feed syrup. Glucose present upstream can contribute to sorbitol formation during hydrogenation, while other carbohydrates may generate additional hydrogenated products.
The second step is maintaining appropriate hydrogenation conditions to achieve high maltose conversion without unnecessary degradation or side reactions.
This is why high-maltose syrup preparation and selective hydrogenation should be engineered together.
Reducing unwanted polyols upstream can lower the burden on downstream purification and improve the economics of producing higher-purity maltitol.
-
-
How can catalyst consumption and hydrogenation operating costs be reduced?
-
Catalyst performance is influenced by feed purity, reaction conditions, impurity accumulation, operating stability, and catalyst management.
Poorly purified feed may shorten effective catalyst life or create unstable hydrogenation performance.
A competitive process therefore considers maltose syrup purification, catalyst protection, hydrogen utilization, reaction selectivity, and continuous operating stability together.
When comparing technologies, customers should ask about catalyst and hydrogen consumption per ton of qualified maltitol—not simply reactor capacity.
-
-
Why is crystallization critical when producing high-purity crystalline maltitol?
-
Crystalline maltitol production places additional demands on feed purity and crystallization control.
Concentration, supersaturation, seeding, cooling profile, residence time, and impurity levels can influence:
- crystallization yield
- crystal size distribution
- centrifugation
- drying performance
- final product consistency
Poor crystallization can leave valuable maltitol in the mother liquor or generate excessive fines.
Myande's evaporation and crystallization engineering capabilities can help optimize purification, concentration, crystal growth, and product recovery as an integrated system.
-
-
How can mother-liquor losses be reduced in crystalline maltitol production?
-
Mother liquor may contain significant recoverable maltitol together with other polyols and impurities.
Simply recycling all mother liquor is not always economical because impurities can accumulate and adversely affect subsequent crystallization and product purity.
An optimized strategy may include controlled recycle, secondary recovery, additional purification, or selective discharge.
The decision should be based on additional maltitol recovery versus purification, evaporation, energy, and wastewater costs, rather than maximizing recycle ratio alone.
-
-
How can evaporation and heat integration reduce maltitol production costs?
-
Concentration may be required at several stages, from maltose syrup preparation to final maltitol concentration and crystallization.
These operations can create substantial thermal demand.
Depending on process conditions, multiple-effect evaporation, MVR or TVR, condensate recovery, and process heat integration can be evaluated to reduce fresh steam consumption.
Myande integrates evaporation with upstream syrup preparation, purification, hydrogenation, and downstream crystallization to optimize the overall plant energy balance rather than individual equipment efficiency.
-
-
How can integrated process design reduce the cost per ton of maltitol?
-
Maltitol production is an interconnected process.
Poor starch conversion affects maltose composition; poor syrup purification can affect catalyst performance; low hydrogenation selectivity increases downstream purification load; and poor crystallization leaves valuable maltitol in the mother liquor.
Myande integrates starch preparation, maltose production, syrup purification, hydrogenation, downstream purification, evaporation, crystallization, drying, utilities, and automation as one complete engineering system.
The objective is to maximize qualified maltitol recovered from each ton of starch while minimizing hydrogen, catalyst, steam, water, chemicals, and product losses.
-
-
What should I compare when selecting a maltitol turnkey plant supplier?
-
Do not compare suppliers only by nominal plant capacity or initial CAPEX.
Request comparable indicators covering:
- starch or maltose syrup consumption
- maltose content and feed specifications
- hydrogenation conversion and maltitol selectivity
- sorbitol and other by-product levels
- overall qualified-product recovery
- catalyst and hydrogen consumption
- achievable maltitol grades
- crystallization yield for crystalline products
- steam, electricity, water, and chemical consumption
- wastewater generation
- automation and hydrogen safety
- pilot validation and industrial scale-up capability
The key question is: How efficiently can the complete plant convert starch into the required maltitol grade at the lowest practical lifecycle cost?
-
Contact Us
Contact us to see how we can help you grow your business.
Find the solution to an optimized future.
Contact Us
Product Information
Quantity
Unit
Piece
Support order samples, customization, wholesale direct, and complete payment. If the product you look for does not have corresponding customized content, pls fill out the form below to contact us, and we will reply ASAP.